Outlook: Regulatory Trends Shaping Packaging Hygiene Standards
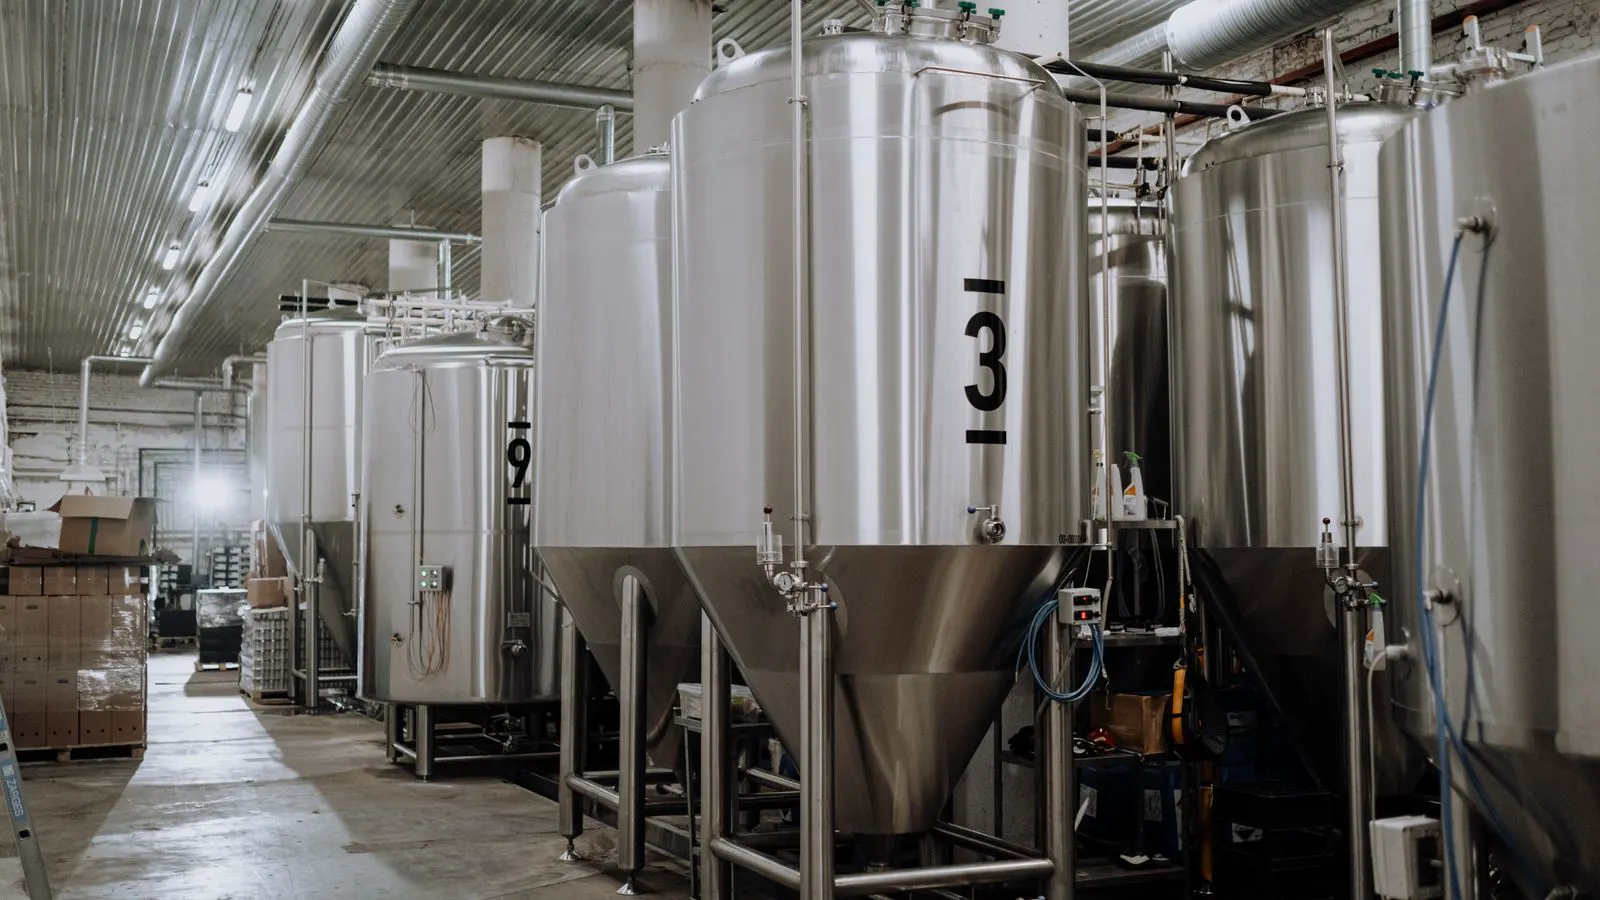
Regulatory updates are moving packaging hygiene standards from basic cleaning to continuous monitoring and digital traceability. Buyers should expect stricter food-grade material rules, tighter CIP validation, and stronger documentation requirements. This article outlines the key shifts and practical steps for preparation.
- Expect tighter requirements around food-grade materials and digital traceability in packaging hygiene standards.
- CIP validation is moving from periodic checks to continuous monitoring and data-driven proof.
- Buyers should plan for stricter documentation, design changes, and staff training to meet upcoming regulatory expectations.
- Early alignment with hygiene standards reduces retrofit costs and audit delays.
- Design and maintenance practices must shift toward continuous hygiene rather than end-of-shift cleaning.
Where the pressure is coming from
Regulatory bodies are tightening expectations around food safety, and the impact is reaching machinery design long before it reaches the production floor. The shift is not about making cleaning harder. It is about proving that cleaning works, that materials stay safe, and that records can be produced quickly during an audit.
For buyers and engineers, this means packaging hygiene standards are no longer just a maintenance topic. They are becoming a design constraint. Machines are expected to support cleaning, inspection, and documentation as part of their normal operation.
The pressure is coming from several directions at once. Food safety regulators want clearer traceability from raw material to finished pack. Customers and retailers want evidence that packaging equipment meets hygiene expectations. Inspectors are asking for records that show how cleaning was verified, not just that it was performed.
This creates a different buying environment. A machine that is fast but hard to clean is less attractive than a machine that is slightly slower but easier to validate. The difference is visible in design choices: gasket placement, drain paths, joint construction, and control features.
Shift one: from visual checks to measured proof
The first major shift is the move from visual inspection to measured proof of cleaning. For a long time, many lines relied on operators checking surfaces by eye and confirming that no visible residue remained. That approach is still common, but it is no longer enough on its own.
Regulators and auditors increasingly expect evidence. That evidence can come from swab tests, ATP checks, residual particle counts, or temperature and time logs from the CIP cycle. The point is to show that the machine reached a defined level of cleanliness, not just that someone looked at it and said it was clean.
This change affects machine design in practical ways. Machines need better access points for swabbing. They need stable surfaces for sampling. They need CIP cycles that can be logged and repeated. They may also need sensors or indicators that confirm rinse quality, temperature, or chemical concentration during cleaning.
For buyers, this means asking for documentation of cleaning validation, not just cleaning instructions. A machine that can demonstrate its cleaning performance over time is easier to defend during an audit.
Shift two: tighter rules for food-grade materials
The second shift is tighter control over food-grade materials. The definition of food-grade is expanding beyond simple stainless steel. Buyers now need to confirm that every part that contacts product, or that could release residues into the product, meets hygiene expectations.
This includes gaskets, seals, lubricants, coatings, fasteners, and even some plastic components. A machine may look compliant on the outside while having a non-compliant seal in a hidden area. Auditors are paying more attention to these details.
The practical impact is that material specifications must be part of the machine selection process. Buyers should ask for material declarations for all contact parts. They should ask for supplier documentation, not just a verbal assurance that parts are food-grade. They should also ask how the supplier handles material changes over time.
A small change in a supplier can create a compliance problem. A new gasket compound, a changed coating, or a different lubricant can alter the machine’s hygiene profile. Machines that allow easy inspection and replacement of these parts are easier to maintain over time.
Shift three: CIP validation becomes a core requirement
The third shift is the elevation of CIP validation from a maintenance task to a core compliance requirement. CIP systems have become common, but regulators are now asking how the system is validated and how often it is verified.
This means that a CIP program is not just a set of steps. It is a documented process with defined parameters, testing points, and review cycles. Buyers need to understand how the machine supports this process. Does the control system log cycle parameters? Can it flag deviations? Can it store records for the required period?
The design implications are significant. Machines need reliable CIP nozzles, proper drainage, and access for inspection. They need controls that can be configured for different products and cleaning agents. They need interfaces that make it easy to record operator actions and system responses.
For buyers, this means evaluating CIP capability as part of the machine decision. A machine with a simple CIP setup may be enough for low-risk products, but a high-speed line with multiple changeovers may need a more capable system. The key is alignment between the cleaning method and the regulatory expectations for the product.
Shift four: digital traceability and audit readiness
The fourth shift is the growing importance of digital traceability. Regulators want to know how a product was handled, cleaned, and packaged. This creates pressure to connect machinery records to broader quality systems.
This does not always mean a full digital transformation. It often means basic digital records: electronic logs, timestamped cleaning cycles, and stored parameter data. But it does mean that paper logs are becoming less acceptable for high-risk products or regulated markets.
Machines that can export cleaning and operation data are easier to integrate into quality systems. They also reduce the risk of missing records during an audit. A paper log can be lost, misfiled, or incomplete. A digital record can be retrieved and reviewed quickly.
For buyers, this is a design and integration question. The machine should support the data needs of the facility. If the facility uses a quality management system, the machine should be able to feed data into it. If the facility uses local data storage, the machine should support that. The goal is not complexity. It is reliability.
Shift five: hygiene by design, not by cleaning
The fifth shift is a move from hygiene by cleaning to hygiene by design. This is one of the most important changes for machinery buyers. It means that hygiene performance is built into the machine from the start, not added through aggressive cleaning at the end of the day.
Hygiene by design focuses on reducing the places where product can hide. It means fewer blind corners, better drainage, simpler joints, and easier access. It means that the machine is built to be clean, not just cleanable.
This is different from the old approach, where a machine could be fast but difficult to clean, and the cleaning team compensated with more effort. That approach is harder to justify when auditors ask for proof of cleaning effectiveness.
For buyers, hygiene by design changes the evaluation process. It means looking at the machine’s layout, not just its speed. It means checking for open drains, removable panels, and easy access to internal parts. It means asking how the machine handles changeovers and whether the design supports rapid cleaning.
What this means for buyers and engineers
These shifts are changing how packaging machinery is selected and maintained. The focus is moving from performance alone to performance plus compliance. A machine must meet production targets while also supporting hygiene validation, material control, and documentation.
Buyers should start by reviewing their current hygiene procedures. They should identify where the weakest points are. Are cleaning records incomplete? Are material declarations missing? Are CIP cycles not fully documented? These gaps will become more visible as regulators tighten expectations.
Engineers should review machine design for hygiene risks. They should look for areas where product can accumulate, where cleaning is difficult, or where records are hard to capture. They should also consider how the machine will age. Seals wear, gaskets change, and materials degrade. A machine that is easy to inspect and maintain over time is more likely to stay compliant.
The practical step is to align machine selection with hygiene requirements. This means asking suppliers for design details, material information, and CIP validation support. It means evaluating the machine as a compliance asset, not just a production asset.
A practical preparation plan
| Area | What to check | Why it matters |
|---|---|---|
| CIP validation | Are cycle parameters logged and repeatable? | Auditors need proof, not just a claim |
| Food-grade materials | Are all contact parts documented? | Material changes can break compliance |
| Drainage and joints | Are blind corners minimized? | Residue hides in hard-to-reach areas |
| Digital records | Can cleaning data be exported? | Paper logs are harder to defend |
| Access and inspection | Are panels removable and swab points clear? | Inspectors need easy access to verify |
| Changeover design | Is changeover time and cleaning effort low? | Rapid changeovers increase hygiene risk |
The plan is simple. Start with the weakest point. Fix it first. Then move to the next. This approach reduces cost and avoids large retrofits later.
- Review current hygiene records and identify gaps in documentation.
- Check material declarations for all contact parts and request updates where needed.
- Evaluate CIP capability and confirm that validation data is stored and accessible.
- Inspect the machine for blind corners, poor drainage, or difficult access points.
- Align machine selection criteria with hygiene requirements before finalizing a purchase.
- Train operators and maintenance staff on the new documentation and inspection expectations.
- Schedule periodic reviews to keep up with changing regulatory expectations.
Final considerations
The direction is clear. Packaging hygiene standards are becoming more demanding, and the impact is reaching machine design and maintenance practices. The goal is not to make compliance harder. It is to make it more reliable.
For buyers, the opportunity is to select machines that are built for hygiene from the start. For engineers, the opportunity is to design systems that make compliance easier to prove. For facilities, the opportunity is to reduce audit risk and avoid costly retrofits.
The best approach is practical. Focus on the areas that matter most. Document the work. Build the capability into the machine selection process. Then review regularly. This is how facilities stay ahead of regulatory changes without being caught off guard.
Frequently asked questions
What is the biggest change in packaging hygiene standards?
The biggest change is the move from visual cleaning checks to measured proof of cleanliness. Auditors now expect documented evidence, such as CIP logs, swab results, or ATP readings, not just operator confirmation.
How does this affect machine design?
Machine design is shifting toward hygiene by design. This means fewer blind corners, better drainage, easier access for inspection, and controls that support cleaning validation and data logging.
What should buyers ask suppliers about materials?
Buyers should ask for material declarations for all food-contact parts, including gaskets, seals, lubricants, and coatings. They should also ask how the supplier handles material changes over time.
Is CIP still enough on its own?
CIP is still a core tool, but it must be validated and documented. Buyers should confirm that the CIP system can log parameters, store records, and support periodic verification.
What is the first step for facilities preparing for these changes?
The first step is to review current hygiene records and identify gaps. Facilities should check documentation, material declarations, and CIP validation to find the weakest points and fix them first.


