Explainer: What Makes Packaging Machinery Food Grade Certified
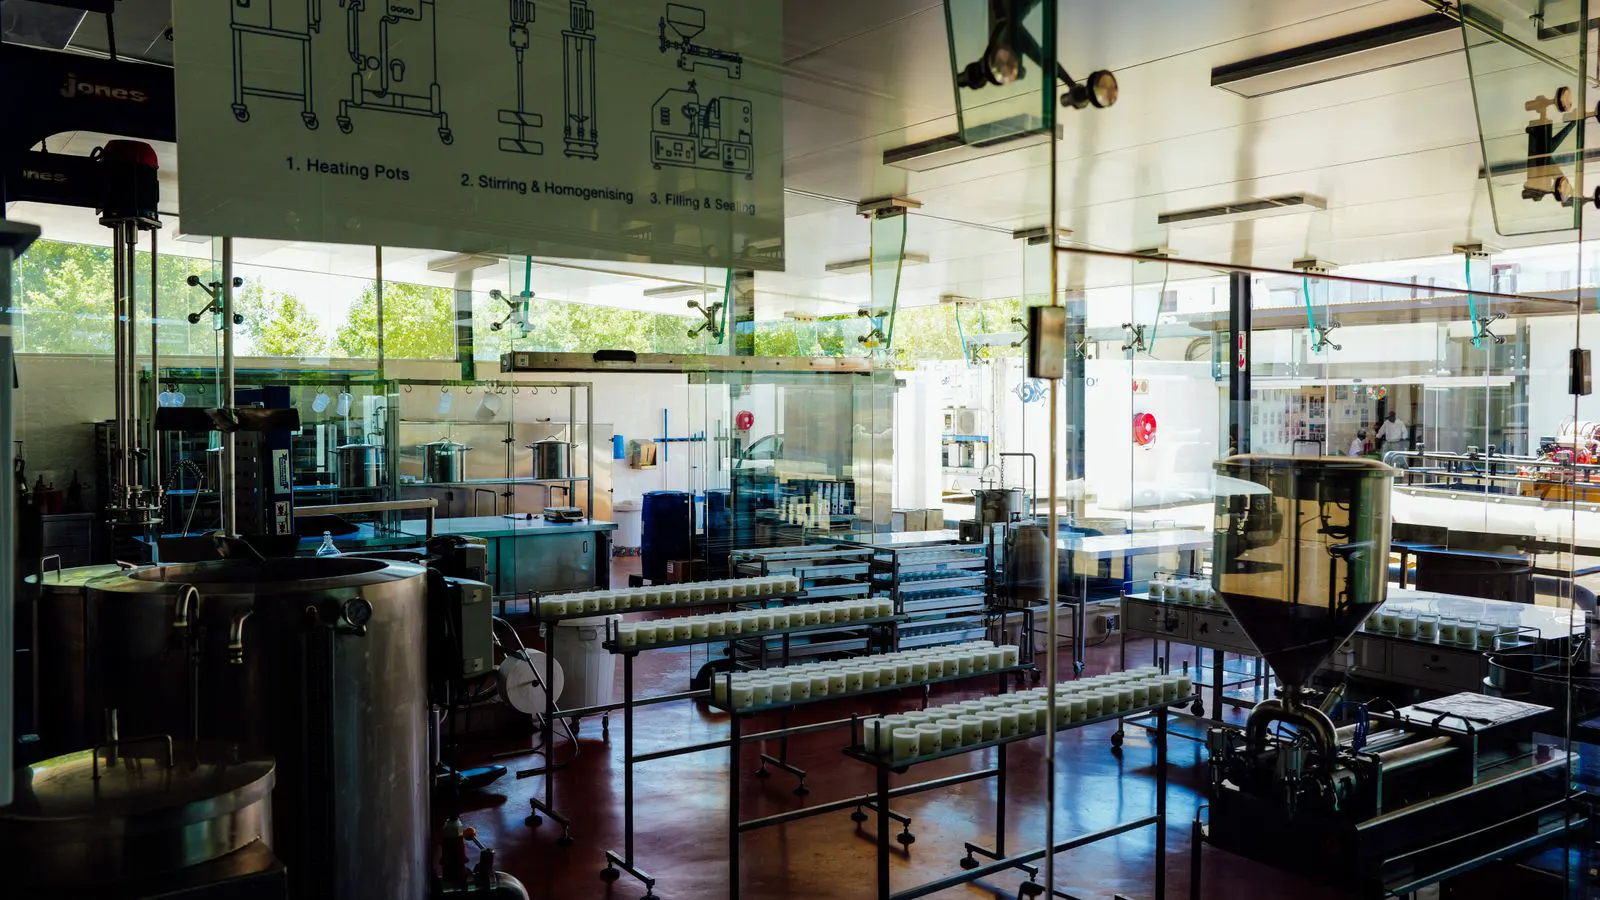
Food grade certified packaging machinery uses compliant materials, smooth surfaces, and specific design features. These elements prevent contamination and meet regulatory standards. Understanding these factors helps buyers source equipment that supports safe production and easier cleaning.
- Food grade certified equipment must use materials that resist corrosion and contamination.
- Hygiene design features like smooth joints and easy cleaning access reduce bacterial growth.
- Certification is a process, not just a label, and it involves third-party audits.
- Buyers should verify specific compliance requirements rather than relying on generic claims.
- Proper design supports both hygiene and operational efficiency in food packaging lines.
What does food grade certified actually mean
The term food grade certified describes packaging machinery that meets specific standards for materials, construction, and cleaning. It is not a single universal stamp. Instead, it refers to equipment that can be proven safe for contact with food or for use in food environments.
When a machine is described as food grade certified, it must pass defined checks. These checks look at the raw materials used in contact zones, the geometry of moving parts, and the ability of the machine to be cleaned without disassembly.
The certification process usually involves a third-party body. That body inspects the machine against a recognized standard. The standard sets rules for surface finish, material composition, and design features.
For buyers, this matters because “food safe” is a marketing phrase. Certification is a documented claim. It provides evidence that the equipment was built to a specific technical baseline.
Materials that define compliance
The base material of the machine is the first line of defense against contamination. Stainless steel is the most common choice for food contact surfaces. The type of stainless steel matters. Different grades offer different levels of corrosion resistance and mechanical strength.
Aluminum is sometimes used in non-contact areas. It is lighter and cheaper than stainless steel. However, it is not typically used where food contact is expected, because it can react with certain food acids.
Plastics and polymers are used in seals, bearings, and conveyor belts. These parts must be food compliant. They should not leach chemicals into the product. They should also resist the cleaning agents used during CIP cycles.
Gaskets and O-rings are a frequent failure point. If a seal is made from a non-compliant polymer, it can introduce contamination even if the main frame is compliant.
The table below shows common materials and their typical roles in food packaging equipment.
| Material | Typical Use | Hygiene Consideration |
|---|---|---|
| Stainless steel | Frame, contact zones, shafts | Must meet food contact standards and resist corrosion |
| Aluminum | Non-contact structural parts | Not suitable for direct food contact in many cases |
| Food-grade plastics | Seals, belts, guides | Must resist leaching and cleaning chemicals |
| Rubber | Gaskets, vibration dampers | Must be compliant and easy to inspect |
| Glass | Seals, viewing windows | Chemically inert but fragile in high-speed areas |
Hygiene design: more than just clean surfaces
Hygiene design is the part of the machine that prevents bacteria from hiding. It is not enough for a surface to be polished. The geometry must allow water and cleaning agents to reach every spot.
Sharp internal corners are a major problem. They trap residue and make thorough cleaning difficult. Compliant designs use rounded transitions. These reduce the chance of product buildup in crevices.
Protruding bolts and threads are another issue. If a bolt head sits on a food contact surface, it creates a shadow zone. That zone can hold moisture and organic matter. Hygiene design requires that fasteners be recessed or covered.
Drainage is a key factor. If liquid pools in a low point, it becomes a breeding ground. Good design includes sloped surfaces and drain channels. These direct liquid away from the product path.
Access points must be easy to open. If a technician has to remove multiple panels to clean a bearing, the cleaning process becomes less consistent. Hygiene design prioritizes quick access. It reduces the time the machine is open to ambient air.
Compliance requirements: what the standard actually checks
Compliance requirements vary by region and industry. Some buyers follow local food authority rules. Others follow international standards set by recognized bodies. The specific standard matters because it defines the test methods.
A typical compliance check looks at several areas. First, it inspects material certificates. The supplier must prove that the steel and polymers meet food contact regulations.
Second, it examines surface finish. Rough surfaces hold more particles. Standards often set limits on surface roughness, especially in contact zones.
Third, it reviews the cleaning design. The auditor will try to clean the machine. They may use water, detergent, and sanitizers. They will check if residue can be removed without damaging the product path.
Fourth, it checks for trapped areas. The auditor looks for gaps, blind holes, and hidden channels. If a residue pocket exists, the machine may fail.
Fifth, it reviews documentation. The buyer should receive a certificate of conformity. This document lists the specific standard used and the scope of the audit.
A common mistake is assuming that any machine from a European manufacturer is automatically compliant. It may be built to local standards, but those standards may not match the requirements of the target market.
How certification affects sourcing decisions
When sourcing food grade certified machinery, the certification status changes the risk profile. An uncertified machine may be cheaper upfront. However, it creates compliance risk. If a customer requires certified equipment, the buyer may face rejection or costly retrofits.
Certification also affects maintenance. Compliant machines are designed with serviceability in mind. They have fewer hidden parts and easier access. This reduces downtime and makes cleaning faster.
The cost difference is not just in the machine price. It includes the cost of audits, documentation, and potential rework. A certified machine may cost more initially, but it simplifies the buying process.
Buyers should ask for the specific standard. For example, if the machine is intended for a market that follows a particular hygiene code, the supplier must confirm that the audit covered that code.
The certification also supports warranty claims. If a part fails, a certified machine has a documented design. This makes it easier to identify whether the failure was a manufacturing defect or a usage issue.
A worked example: verifying a packaging line
Imagine a buyer purchasing a vertical form fill seal machine for packaged snacks. The buyer needs the machine to handle high-speed operation and meet hygiene requirements.
The supplier offers a machine with a stainless steel frame. The buyer asks for material certificates. The supplier provides mill test reports for the steel. The reports confirm the grade meets food contact rules.
The buyer then reviews the design. They notice that the filler nozzles have smooth, rounded transitions. There are no exposed threads on the product side. The conveyor belt is made from a food-grade polymer.
The buyer asks for the cleaning procedure. The supplier provides a CIP protocol. The protocol includes specific temperatures and chemical concentrations. It also lists the access points for manual cleaning.
The buyer requests a third-party audit report. The report shows that an independent body inspected the machine. The body confirmed that the design meets the required hygiene standard.
During the on-site review, the buyer checks the seals. They find that the gaskets are made from a compliant material. They also check the drain points. They confirm that water can flow freely from the contact zones.
The buyer also reviews the documentation package. It includes the certificate of conformity, the material certificates, and the cleaning instructions. This package is complete.
The buyer signs the purchase order. The machine arrives, and the buyer performs an initial cleaning test. They find that the machine cleans as expected. The documentation matches the physical machine.
This example shows that certification is not a single event. It is a chain of evidence. Each link must hold for the buyer to trust the claim.
Common pitfalls to avoid
One common mistake is confusing “food grade” with “food contact.” Some parts of a machine may be food grade, but they are not in direct contact with the product. The buyer must clarify which parts are certified and which are not.
Another mistake is accepting a generic statement. If a supplier says the machine is “hygienic,” the buyer should ask for the specific standard. A vague claim does not provide enough information for a compliance decision.
A third mistake is ignoring the cleaning system. A machine may be well-designed, but if the cleaning system is inadequate, the hygiene goal fails. The buyer should evaluate the CIP system as part of the overall package.
A fourth mistake is not checking the supplier’s track record. A supplier that has only a few certified machines may have limited experience. A supplier with a long history of food equipment may be more reliable.
A fifth mistake is not planning for maintenance. Certification is not permanent. If a part is replaced with a non-compliant substitute, the certification can be void. The buyer must ensure that spare parts are also compliant.
What to ask suppliers before purchase
Before signing a contract, buyers should ask a structured set of questions. These questions help separate genuine compliance from marketing language.
- What specific standard does the machine meet for food contact?
- Can you provide material certificates for all food contact parts?
- What is the surface finish specification for contact zones?
- How is the machine cleaned, and what is the expected cleaning time?
- What documentation will you provide after installation?
- Are spare parts included in the certification scope?
- Can you provide references from customers in similar industries?
These questions force the supplier to be specific. A supplier that cannot answer them clearly is a red flag.
The buyer should also verify that the standard is recognized in their target market. A standard that is valid in one country may not be accepted in another.
The final decision should be based on evidence, not promises. The documentation, the design, and the audit report form the basis for the purchase.
Frequently asked questions
Is food grade certification the same as food contact certification?
Not always. Food grade certification often refers to the overall machine design and cleaning. Food contact certification focuses on specific materials that touch the product.
Can a machine lose its food grade certification?
Yes. If parts are replaced with non-compliant materials or if the machine is modified without re-inspection, the certification may be void.
Do I need a third-party audit for every machine?
It depends on your market and customer requirements. Many buyers require a third-party audit to confirm compliance, especially for export markets.
What is the difference between hygiene design and food grade certification?
Hygiene design is the set of features that prevent contamination. Food grade certification is the formal confirmation that the machine meets a specific standard, which includes hygiene design.
How long does the certification process take?
There is no fixed time. It depends on the complexity of the machine and the auditing body. Some audits take days, others take weeks.


