OEM vs Third-Party Parts: Cost and Lead Time Impact
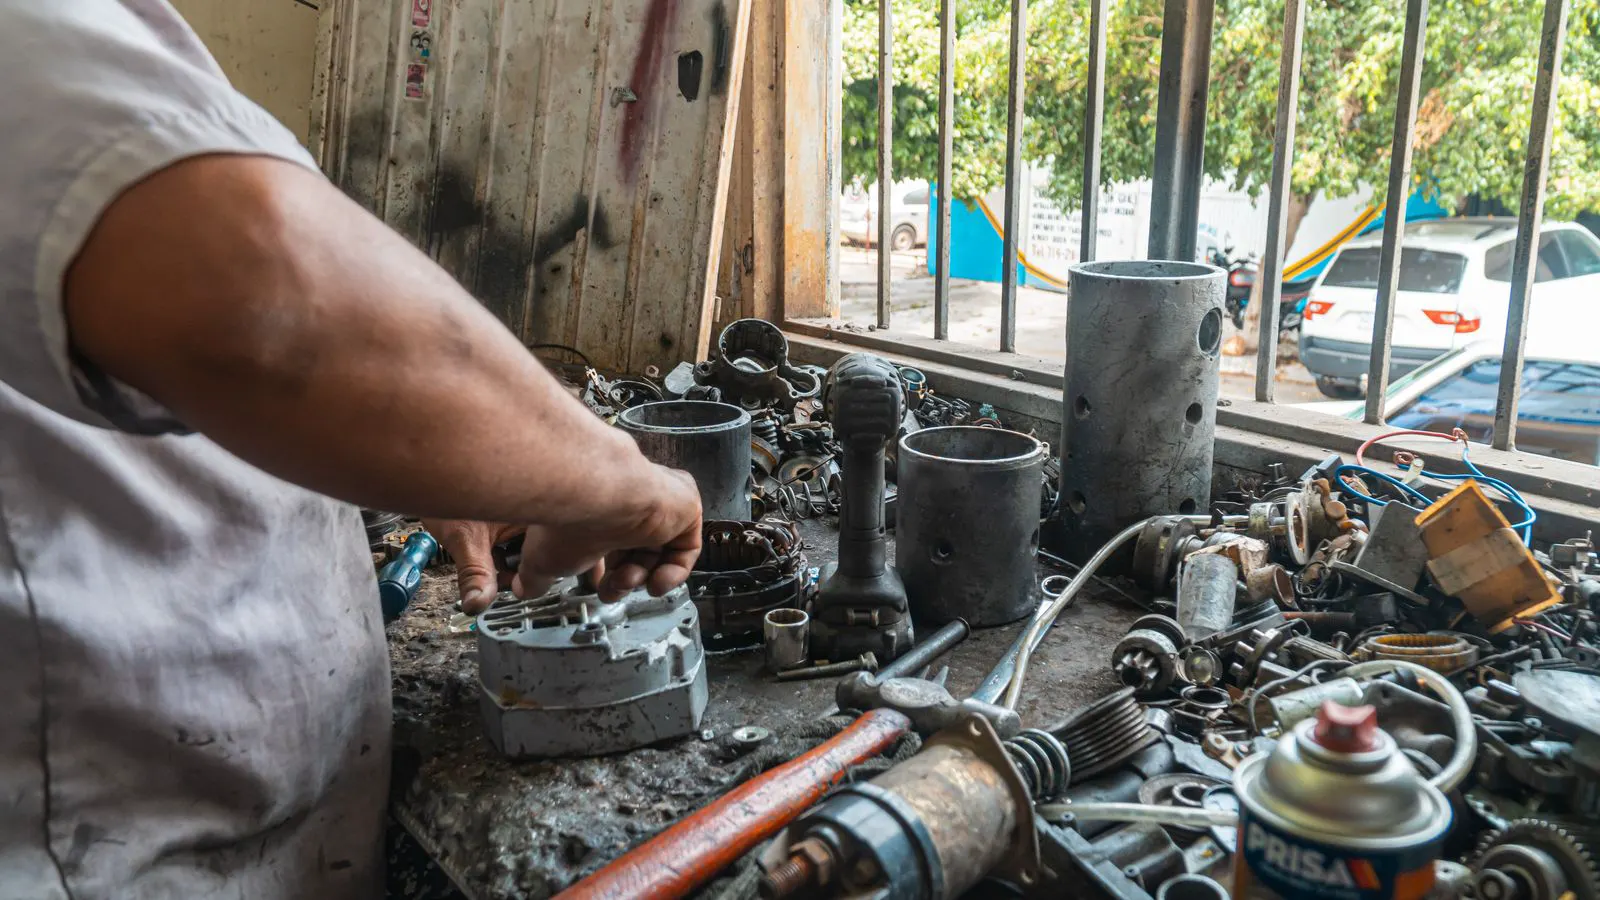
Choosing between OEM and third-party spare parts cost depends on line criticality, part availability, and fit. OEM parts offer guaranteed compatibility but often carry higher prices and longer wait times. Third-party options can reduce spend if specifications match exactly.
- OEM parts usually cost more and can take longer, but they reduce fit risk.
- Third-party parts lower purchase cost only when dimensions, materials, and specs match.
- Lead time affects downtime cost, not just the invoice price.
- Keep a parts list for critical items and test replacements before full rollout.
- Track operating cost by including labor, verification, and scrap risk, not just part price.
What drives the real cost of a spare part
A replacement part price is only one number on a purchase order. The true cost includes downtime, labor, verification, and the risk of a second failure. On a packaging line, a missing or incorrect part can stop a shift. The cost of that stoppage often outweighs the part itself.
When you compare sources, the first question is whether the part is a commodity or a proprietary component. Bearings, gaskets, sensors, and standard fasteners often have multiple suppliers. Proprietary drives, control boards, and custom tooling may have only one source. The sourcing strategy changes based on that distinction.
A line that runs twenty-four hours a day carries a different risk profile than one that runs two shifts. A single missing seal can force a shutdown, and the cost per hour of idle time rises quickly. The spare parts budget should reflect that exposure.
How OEM sourcing affects price and schedule
Original equipment manufacturer parts come from the machine builder or their approved supplier. They are made to the original drawings. The price usually reflects that guarantee.
OEM parts often cost more. The markup covers engineering support, quality documentation, and the brand. The lead time is not always predictable. A part that is in stock at a local dealer may not be in stock at your region’s warehouse. A custom tooling item can take weeks or months to produce.
For critical components, the cost of a mismatched part can be higher than the price difference. A seal with the wrong durometer can leak. A sensor with the wrong voltage can damage a controller. A bearing with the wrong load rating can fail early. The failure may require a full teardown.
OEM sourcing also simplifies records. The part number matches the machine documentation. The service history stays clean. Auditors and buyers can see a clear chain of custody.
How third-party sourcing changes the equation
Third-party parts are made by independent suppliers. They may be generic replacements or reverse-engineered components. The purchase price is often lower. The risk is fit.
The first check is the drawing or datasheet. Dimensions, material grade, tolerance, and finish matter. A bolt that looks the same may have the wrong thread pitch. A hose that fits may not handle the same pressure or temperature. A sensor that fits the mounting may output a different signal.
Third-party sourcing works well for standard items. A set of bearings for a conveyor roller is a good example. A gasket set for a common housing is another. The buyer can verify the part against a known good unit before installation.
For proprietary items, third-party sourcing is riskier. A control board replacement may require firmware matching. A custom drive may need calibration. The supplier may not support the part after installation. If the part fails, the buyer may be left to troubleshoot alone.
Lead time varies by supplier. A local distributor can ship a standard part the next day. A remote manufacturer may ship in two weeks. A custom part may take longer than expected. The buyer should confirm the production date and the shipping method before ordering.
Comparison of sourcing options
| Option | Best for | Limitations |
|---|---|---|
| OEM parts | Critical components, warranty-sensitive lines, proprietary items | Higher price, possible longer lead time, single source |
| Third-party generic parts | Standard bearings, seals, gaskets, fasteners | Fit risk, limited support, quality variability |
| Authorized distributor stock | Common parts, urgent repairs, predictable lead time | May not carry niche items, price can vary by region |
| Reverse-engineered custom parts | Discontinued components, niche tools | Longer production time, higher engineering cost, fit uncertainty |
| Machine builder service contract | Full line coverage, reduced internal labor | Higher recurring cost, less control over parts selection |
When to choose OEM parts
Choose OEM parts when the component is safety-related or when a failure stops the line. A drive motor, a control board, or a pressure regulator may fit this category. The price premium is easier to justify when the risk of a mismatch is high.
OEM parts are also the right choice when the machine is under warranty. Installing a non-OEM part can void coverage. The buyer should check the warranty terms before deciding. If the warranty covers the line for three years, a cheap third-party seal may cost more if it fails and voids a repair claim.
For new lines, OEM parts give a baseline. The buyer knows the part works in the machine. The service team knows the part. The parts list is clear. After the line is stable, the buyer can shift some standard items to third-party sources.
When to choose third-party parts
Choose third-party parts for standard items that are easy to verify. Bearings are a good example. The inner diameter, outer diameter, width, load rating, and seal type are published. The buyer can match the part to the machine drawing.
Seals are another area where third-party parts can work. The seal size, material, and hardness must match. The buyer should compare the material grade to the original. A nitrile seal may not handle the same chemical exposure as a fluoropolymer seal. The failure mode may be slow, not sudden.
Fasteners and small hardware are often interchangeable. A bolt that fits the thread may not have the same grade. The grade affects strength and fatigue life. The buyer should check the material grade on the part.
A good practice is to keep a small stock of third-party standard parts. The stock should be based on failure history, not guesswork. If a conveyor bearing fails every six months, the stock should reflect that. If a sensor fails once a year, the stock can be smaller.
How lead time affects operating cost
Lead time is not just a shipping date. It is the time between a failure and a working part. That window includes diagnosis, teardown, part search, shipping, and installation.
A part that costs less but arrives in three weeks may cost more than a part that costs more but arrives in two days. The buyer should calculate the cost of downtime per hour. Then compare the part price to the downtime cost.
A line that runs twenty-four hours a day has a high downtime cost. A line that runs two shifts has a lower cost. A line that runs one shift has the lowest cost, but the downtime still affects the production plan.
The lead time strategy should match the part criticality. A critical part should have stock on site. A standard part can be ordered from a distributor. A custom part may need a longer lead time and a higher price.
How to verify a third-party part before installation
Verification happens before the part goes on the line. The buyer should compare the part to the original or a known good unit. The check list should include dimensions, material, finish, and markings.
For mechanical parts, the check is physical. A bearing should have the same dimensions and load rating. A gasket should have the same thickness and material. A fastener should have the same grade and thread.
For electrical parts, the check is electrical. A sensor should have the same output signal and voltage. A relay should have the same contact rating. A drive should have the same torque and control interface.
The buyer should test the part in a safe environment if possible. A seal can be tested for pressure. A sensor can be tested with a signal generator. A drive can be tested with a load. The test should be documented.
If the test fails, the part should not go on the line. The cost of a failed part is higher than the cost of a returned part. The buyer should have a return process in place. The supplier should accept returns for defective or incorrect parts.
How to track operating cost and improve the parts strategy
The parts strategy should be reviewed after a quarter. The buyer should look at the data. Which parts failed most often? Which parts had the longest lead time? Which parts caused the most downtime?
The data should include the part number, the supplier, the price, the lead time, and the installation time. It should also include the downtime cost and any scrap cost. The total cost is the sum of these items.
A part that is cheap to buy but expensive to install may not be a good deal. A part that is expensive to buy but installs quickly may be a better choice. The buyer should look at the total cost, not just the invoice.
The parts list should be updated after major maintenance. If a part was replaced with a different design, the new part number should be added. If a part was found to be faulty, the failure reason should be recorded. The data helps the buyer make better decisions.
The strategy should be simple. Keep critical parts in stock. Use OEM parts for proprietary items. Use third-party parts for standard items. Verify every part before installation. Track the cost and adjust the strategy based on the data.
Common mistakes to avoid
The first mistake is buying the cheapest part without checking the specs. A part that looks right may not work. The failure may happen weeks later, when the line is under pressure.
The second mistake is ignoring lead time. A part that is in stock but from a remote supplier may arrive too late. A part that is not in stock but from a local supplier may arrive in time. The buyer should check the stock level before ordering.
The third mistake is not documenting the part change. If a part is replaced with a different design, the documentation should be updated. The service team should know the part. The parts list should be current.
The fourth mistake is not testing the part. A part that has not been tested may fail in the field. The test should be done in a safe environment. The test should be documented.
The fifth mistake is not tracking the cost. Without data, the buyer cannot make a good decision. The data should include the part price, the lead time, the installation time, and the downtime cost.
Final note on sourcing strategy
The sourcing strategy should match the part and the line. Critical parts should be sourced from a trusted supplier. Standard parts can be sourced from multiple suppliers. The buyer should verify every part. The buyer should track the cost. The buyer should adjust the strategy based on the data.
A good parts strategy is not about buying the cheapest part. It is about buying the right part at the right time. The cost includes the downtime, the labor, and the risk. The buyer should look at the total cost, not just the invoice.
The parts strategy should be reviewed after a quarter. The buyer should look at the data. The buyer should update the parts list. The buyer should adjust the stock levels. The buyer should choose the right supplier for each part.
Frequently asked questions
How do I know if a third-party part is safe to use?
Verify the part against the original drawing or a known good unit. Check dimensions, material, tolerance, and finish. Test the part in a safe environment before installation.
Can I use third-party parts without voiding the warranty?
Check the warranty terms before installing any non-OEM part. Some warranties cover the line, and some cover the parts. A non-OEM part may void coverage if it causes a failure.
What is the best way to reduce spare parts cost?
Keep a stock of critical parts. Use third-party parts for standard items. Verify every part before installation. Track the total cost, not just the invoice price.
How long should I keep spare parts in stock?
Keep stock based on failure history and lead time. A part that fails often should have more stock. A part that fails rarely should have less stock. The stock should cover the lead time plus a buffer.
What should I do if a part fails after installation?
Document the failure. Return the part to the supplier if it is defective. Check the installation and the part spec. Update the parts list and the maintenance plan.