Buyer Guide: Sizing Packaging Machines for High Volume
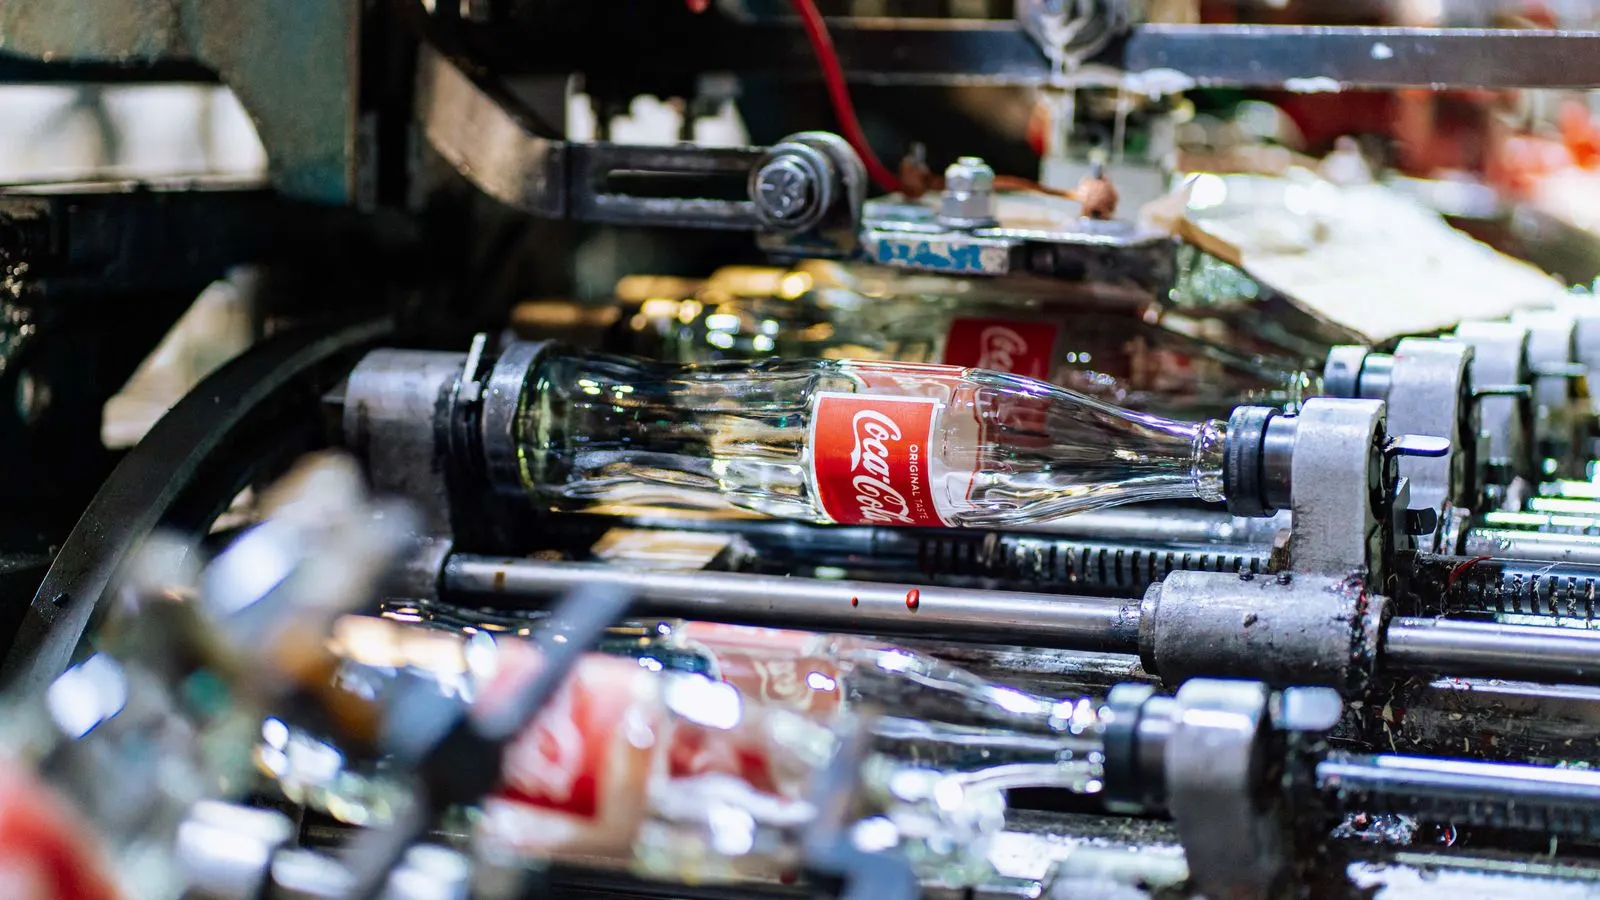
Determine production volume first. Match machine throughput to actual demand, account for cycle times and changeovers, and verify capacity planning against peak seasons to avoid bottlenecks in high-volume packaging.
- Calculate peak demand, not just average demand, when evaluating production volume for new lines.
- Machine capacity must match line speed to prevent bottlenecks and idle time.
- Account for changeover time and downtime in capacity planning to ensure realistic output.
- Verify that auxiliary equipment matches the main machine's throughput requirements.
- Use a decision checklist to confirm all sizing parameters before purchasing high-volume equipment.
High-volume packaging lines fail when equipment sizing lags behind actual production demand. A machine rated for a certain output may struggle when changeovers, maintenance, and material feed issues compound over a shift. Buyers need to evaluate production volume through multiple lenses to select machinery that performs consistently.
This guide walks through the practical steps for sizing packaging machines for large-scale operations. It covers demand analysis, throughput calculation, capacity planning, and the criteria that determine whether a machine will hold up over time.
Define Your Actual Production Volume Requirements
Start with the numbers on your floor, not the vendor brochure. Production volume is not just units per hour. It is the total output required across all SKUs, shifts, and seasonal peaks. Many buyers underestimate this by looking at average daily output and ignoring the peaks.
Pull three years of historical data if available. Identify the highest quarterly demand, the highest monthly demand, and the single-day maximum. These figures form the baseline for machine sizing. If your facility plans to grow, add a realistic buffer to these numbers. A typical buffer range is 10 to 25 percent above peak demand, depending on growth forecasts and market volatility.
Distinguish between unit output and weight or volume output. A 500 mL bottle and a 1 L bottle both count as one unit, but they consume different amounts of product and require different cycle times in filling operations. Your machine sizing must reflect the product mix, not just the count.
Calculate Throughput and Line Speed
Throughput and line speed are related but distinct. Line speed is the physical rate at which products move along the line, measured in units per minute or per hour. Throughput is the net output after accounting for stoppages, rejects, and changeovers.
A machine may be rated at 12,000 units per hour at line speed. If changeovers take 45 minutes and maintenance windows consume another 30 minutes per shift, the net throughput drops. This gap between rated capacity and actual throughput is where most capacity planning errors occur.
Use this formula as a starting point:
Net throughput = Rated capacity minus downtime losses.
Downtime losses include changeover time, material jams, quality checks, and preventive maintenance. Track these on your current line for at least two weeks. Multiply the average downtime by your production hours to estimate true capacity.
When comparing machines, ask vendors for both rated speed and realistic throughput at your specific product size. A machine that runs fast with small products may slow down significantly with larger, heavier, or irregularly shaped items.
Account for Changeover Time and Product Flexibility
High-volume lines often run multiple SKUs per shift. Changeover time directly reduces net production volume. A 20 minute changeover per product run eats into a 24 hour shift. Over 10 SKUs, that is 3 hours lost to changeovers alone.
Evaluate machine changeover characteristics carefully. Look for quick-change tooling, modular components, and digital recipes that store settings for each product. Some machines allow changeovers in under 5 minutes. Others require 30 or more. The difference is significant at high volume.
Product flexibility also affects sizing. If your product range spans multiple sizes, shapes, or materials, the machine must accommodate each without major reconfiguration. A rigid machine may handle one product well but fail on others. Flexible machines often cost more upfront but reduce total line cost when running diverse products.
Consider the number of changeovers per day. If you run 30 SKUs in a single shift, the machine must handle rapid transitions. If you run 3 SKUs per shift, changeover time matters less, and you can prioritize peak speed on those few products.
Evaluate Capacity Planning for Peak and Off-Peak Periods
Capacity planning means matching machine output to demand across the year. Off-peak periods may require only 60 to 70 percent of peak capacity. Running a machine at full speed during slow months wastes energy and accelerates wear. Running it at low speed during peak months creates bottlenecks.
Design the line with variable speed capability. Machines with adjustable line speed allow operators to match output to demand in real time. This reduces the need for multiple machines and keeps the line efficient across demand fluctuations.
Plan for seasonal peaks. If your product demand surges during holiday seasons, the machine must handle that surge without additional shifts or overtime. If your demand is stable year-round, you can size closer to average demand with a smaller buffer.
Include utility capacity in the plan. High-volume machines draw significant power, compressed air, and cooling. Verify that your facility infrastructure can support the machine at full speed. An undersized power supply or air compressor creates intermittent stoppages that reduce throughput.
Key Criteria for Selecting High-Volume Packaging Machinery
The table below summarizes the main criteria to evaluate when sizing packaging machines for high-volume production.
| Criterion | What to look for | Why it matters |
|---|---|---|
| Rated throughput | Units per hour at your product size and line speed | Determines if the machine meets peak demand |
| Changeover time | Minutes per SKU transition, with quick-change tooling | Affects net output and flexibility across SKUs |
| Line speed range | Adjustable speed from low to rated maximum | Allows matching output to demand fluctuations |
| Reliability data | Mean time between failures and maintenance intervals | Predicts downtime and long-term throughput |
| Product compatibility | Range of sizes, shapes, and materials supported | Ensures the machine handles your full product mix |
| Integration capability | Compatibility with existing PLCs, SCADA, and upstream/downstream equipment | Prevents bottlenecks and simplifies line control |
Check each criterion against your specific production profile. A machine that scores high on rated throughput but poorly on changeover time may deliver worse net output than a slightly slower machine with fast changeovers.
Verify Integration and Auxiliary Equipment Matching
The main machine is only one part of the line. Fillers, cappers, labelers, case packers, and palletizers must all operate at compatible speeds. If the filler runs at 10,000 units per hour but the capper maxes out at 8,000, the capper becomes the bottleneck. The entire line slows to 8,000.
Review the speed ratings of every machine in the line. Match them as closely as possible. Where speeds differ, identify the limiting machine and plan around it. Sometimes it is cheaper to add a buffer conveyor or a small accumulation area than to replace a slow machine.
Check material flow. High-volume lines require consistent feeding. Infeed systems must deliver product at the right rate without jams or gaps. Outfeed systems must handle product without congestion. These auxiliary components directly affect actual throughput.
Verify control system integration. Modern high-volume lines use centralized control. The main machine should communicate its status, speed, and fault codes to a central system. This allows operators to monitor the entire line from one dashboard and respond quickly to stoppages.
Build a Decision Checklist Before Purchase
Use this checklist to confirm that your machine sizing is correct before signing a purchase order.
- Peak production volume calculated for all SKUs and shifts.
- Net throughput verified after changeover and downtime losses.
- Line speed range matches demand fluctuations across the year.
- Changeover time tested or verified for your fastest-changing SKUs.
- Product compatibility confirmed for your full size and shape range.
- Auxiliary equipment speeds matched to the main machine.
- Facility utilities (power, air, cooling) verified for full-speed operation.
- Control system integration planned with existing line infrastructure.
- Maintenance access and spare parts availability reviewed.
- Long-term growth buffer included in the sizing calculation.
If you cannot check every box, identify which gaps are acceptable and which are deal-breakers. Some items, like utility capacity, must be resolved before installation. Others, like spare parts availability, can be addressed through service agreements.
Final Thoughts on High-Volume Machine Sizing
Production volume is the starting point, but it is not the whole story. A correctly sized machine balances peak demand, changeover time, line speed, and product flexibility. Buyers who treat capacity planning as a single number often end up with machines that are too slow, too rigid, or too costly.
Run the numbers. Test the assumptions. Verify that every part of the line can keep up with the main machine. The result is a line that handles large-scale production without surprises.
Frequently asked questions
How much buffer should I add to peak production volume when sizing a machine?
A typical buffer ranges from 10 to 25 percent above peak demand. The exact amount depends on growth forecasts, product mix changes, and how much downtime you can absorb during peak periods.
Can I use average daily output to size a high-volume machine?
No. Average output hides the peaks that drive equipment requirements. Always use peak quarterly, monthly, and daily figures to size the machine, then adjust for changeover and downtime losses.
What is the difference between rated throughput and net throughput?
Rated throughput is the manufacturer's maximum output under ideal conditions. Net throughput is the actual output after accounting for changeovers, jams, maintenance, and quality checks. Always plan around net throughput.
How do I handle multiple SKUs on a single high-volume line?
Evaluate changeover time and product compatibility. Look for quick-change tooling, modular components, and digital recipes. If changeover time is high, consider whether a second machine or a dedicated line makes more sense.
Do I need to match every machine on the line to the same speed?
Match speeds as closely as possible to avoid bottlenecks. If speeds differ, identify the limiting machine and plan around it with buffer conveyors or accumulation areas rather than replacing equipment.


